A. Loading diagram and design data
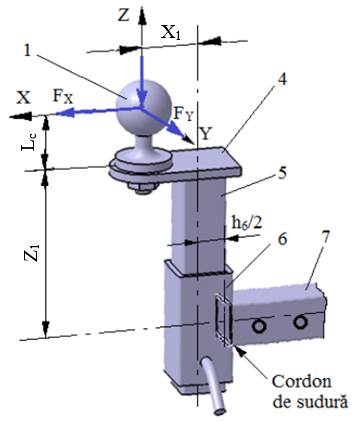
External loading diagram
|
Loading diagram of joint 6-7 |
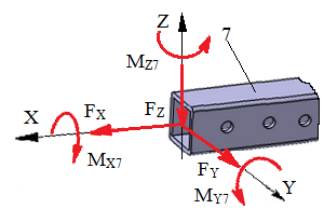 | |
Design data External forces: FX, FY, FZ act at distances Lc (Ex.3.1), X1, X2, Z1 (Ex.1.2.2) and h6 (Ex.4.1); the moments at the centre of the square section are calculated (Calc.0): MX7 = FY (Lc + Z1), MY7 = FX (Lc + Z1) + FZ (X1 + h6/2), MZ7 = FY (X1 + h6/2). Dimensional constraints: the upper column body 6 is welded to the lower tie rod 7, with sizes h6, h7 and wall thicknesses t6, t7 (Ex.4.1, Ex.4.3). Operating constraints: temperature T = (−30…40) °C; outdoor working environment with high humidity. Design constraints: weldable materials for elements 6 and 7. | |
B. Choice of material and heat treatments
Elements 6 and 7 were designed using weldable steels (Ex.4.3). These steels are not heat-treated before welding; after welding, the subassembly may undergo stress-relief annealing. For the adopted steels, the yield strengths σ02 and the ultimate tensile strengths σr are retained for the calculations.
C. Design of the constructive shape
Constructive model
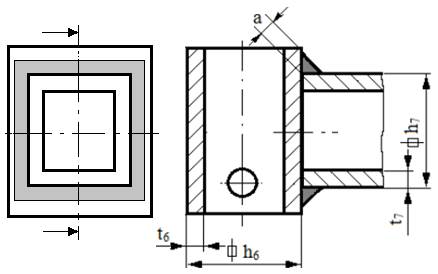
Constructive features and constraints
– the weld throat thickness a should be smaller than the wall thicknesses t6 and t7 of the square tubes (a < min(t6, t7));
– the two elements must be perpendicular;
– a fillet weld is made along the closed (square) contour.
D. Calculation model, sizing and checking
The calculation model is similar to the one in Sec.3.5.
Calculation data
– loading: FXs = FZ, FYs = FX, FZs = FY; MXs = MZ7; MYs = MX7; MZs = MY7;
– shape and dimensions: the inner contour of the weld bead is a square of side h = h7;
– materials: σ02 – the yield strength; c = 2…3 – the safety factor; σat = σ02/c – the allowable tensile stress; τafs = (0.6…0.7)σat – the allowable shear stress of the weld.
Sizing
The weld throat thickness anec is determined with calculation window Calc.3.5.1; a whole value a > anec is adopted.
E. Design of the technological shape
Constructive-technological drawing
|
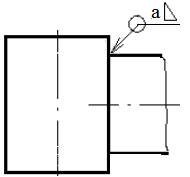
Recommendations for choosing the dimensions and constructive-technological parameters: – weld throat thickness, a; – the weld is made along the closed contour (as symbolised); – after welding, the subassembly undergoes stress-relief annealing. |