A. Loading diagram and design data
External loading diagram
|
Loading diagram of the welded joint 4-5 |
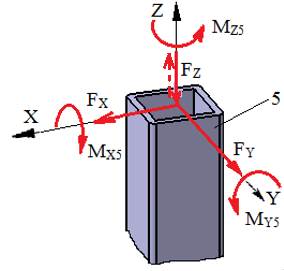 | |
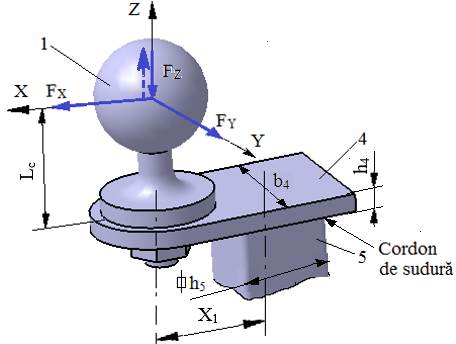
Design data External forces: FX, FY, FZ act at distances Lc (Ex.3.1, Ex.3.2) and X1 (Ex.1.2.2); the moments at the centre of the square section (the welded joint) are calculated (Calc.0): MX5 = FY (Lc + h4), MY5 = FX (Lc + h4) + FZ X1, MZ5 = FY X1. Dimensional constraints: the upper tie rod 4, of width b4 and thickness h4 (Ex.3.1), is welded to the square tube 5 of side h5 and wall thickness t5. Operating constraints: temperature T = (−30…40) °C; outdoor working environment with high humidity. Design constraints: weldable materials for elements 4 and 5. | |
B. Choice of material and heat treatments
Elements 4 and 5 were designed using weldable steels (Annex.M.01). These steels are not heat-treated before welding; after welding, the subassembly may undergo stress-relief annealing. For the adopted steels, the yield strength σ02 and the ultimate tensile strength σr are retained for the calculations.
For the weld bead, the allowable shear stress corresponding to weldable steels is adopted: τafs = (0.6…0.7)σat.
C. Design of the constructive shape
Constructive model
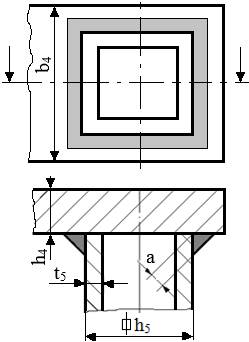
Constructive features and constraints
– the weld throat thickness a should be smaller than the wall thickness t5 of the square tube (a < t5);
– the two elements must be perpendicular;
– a fillet weld is made along the closed contour (square section).
D. Calculation model, sizing and checking
Calculation model
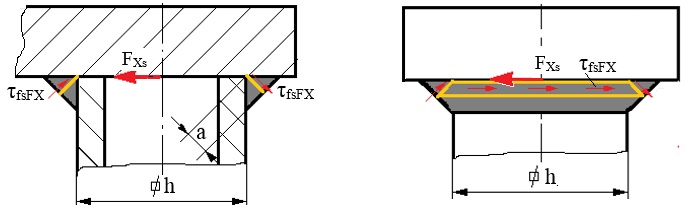
a
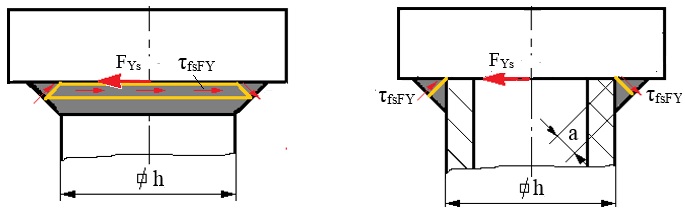
b
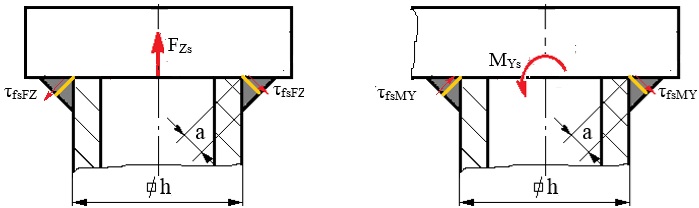
c d
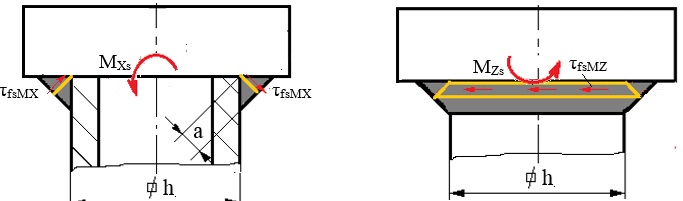
e f
Calculation assumptions and loads
– the external loading consists of the forces FX, FY, FZ and the moments MX, MY, MZ;
– the shear stresses are uniformly distributed along the weld bead in the longitudinal and transverse planes: fig. a for the force FXs, fig. b for FYs, fig. c for FZs, fig. d for the moment MYs, fig. e for MXs and fig. f for MZs;
– the tensile and bending stresses in the weld bead are neglected.
Calculation data
– loading: FXs = FX, FYs = FY, FZs = FZ; MXs = MX5; MYs = MY5; MZs = MZ5;
– shape and dimensions: the inner contour of the weld bead is a square of side h = h5;
– materials: σ02 – the yield strength; c = 2…3 – the safety factor; σat = σ02/c – the allowable tensile stress; τafs = (0.6…0.7)σat – the allowable shear stress of the weld.
E. Calculation relations
– Shear strength condition of the weld
The shear stresses generated by FXs, FYs, FZs, MXs, MYs, MZs (figs. a, b, c, d, e and f, respectively) are:
τfsFX =  , τfsFY =
 , τfsFZ =
 , τfsMX =
 , τfsMY =
 and τfsMZ =

They are added vectorially (for the most unfavourable case, considering that the forces and moments can act in both directions), giving the maximum shear stress at a corner of the square,
τfsmax = 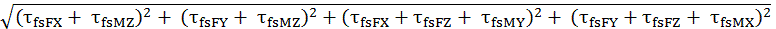 =
= 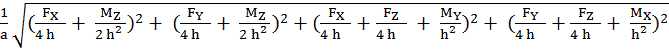 ≤ τafs.
– Sizing the weld
From the relation above (last part), the weld throat thickness is obtained,
anec = 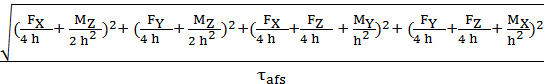 , (Calc.3.5.1)
where τafs is the allowable shear stress of the weld; a whole value a > anec is adopted.
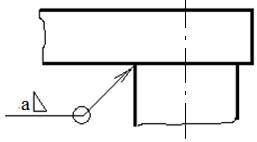
F. Design of the constructive-technological shape
Constructive-technological drawing
|
Recommendations for choosing the dimensions and constructive-technological parameters: – weld throat thickness, a; – the weld is made along the closed contour (as symbolised); – after welding, the subassembly undergoes stress-relief annealing. |