Design data
External forces: FX = 1500 N.
Dimensional constraints: the square tube 7, of side h7 = 50 mm and thickness t7 = 5 mm, is assembled with the square tube 8, of side h8 = 60 mm and thickness t8 = 5 mm.
Operating constraints: temperature T = (−30…40) °C; outdoor working environment with high humidity.
Design constraints: dimensional interchangeability.
Materials and heat treatments
A weldable material, S235 steel according to SR EN 10025-2 (STAS 500/2), was chosen for elements 7 and 8.
The pin is made of a steel for mechanical construction, e.g. E295 (SR EN 10025/2005).
Material properties
| Material | Heat treatment | Hardness [HB] | Yield strength | Ultimate tensile strength, σr |
|---|---|---|---|---|
| S235 | – | – | σ02 = 235 MPa | σr = 360 MPa |
| E295 | – | – | σ02 = 295 MPa | σr = 390 MPa |
Allowable shear stress τaf = 60 MPa.
Allowable steel-on-steel crushing stress σas = 70 MPa.
Sizing and checking
Sizing
From the sizing relation obtained from the crushing strength conditions of the pin joint, with F = FX = 1500 N, ti = t7 = 5 mm, te = t8 = 5 mm and σas = 70 MPa, the required pin diameter is
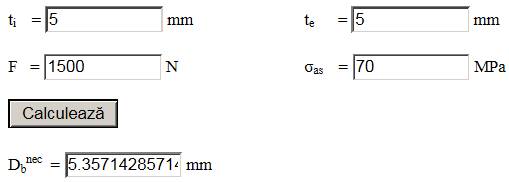
Db = 10 mm is adopted.
Checking
The shear stress in the pin, with F = 1500 N and Db = 10 mm, is
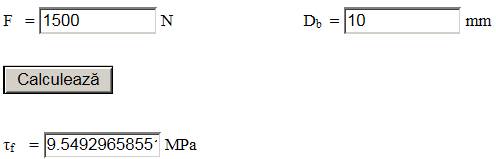
and the check τf ≤ τaf becomes 9.55 ≤ 60 MPa (satisfied).
Constructive-technological shape
Constructive-technological drawing
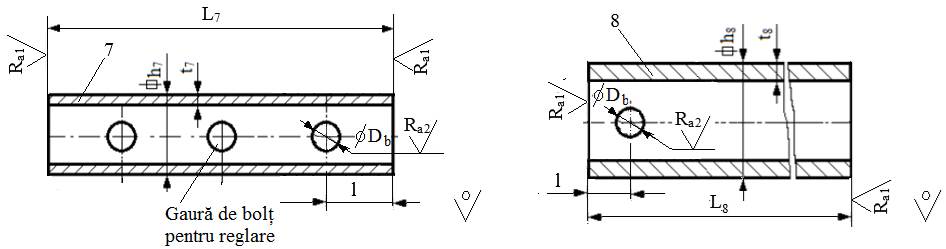
Adopted constructive-technological parameters
– dimensions: h7 = 50 mm, t7 = 5 mm, h8 = 60 mm, t8 = 5 mm, L7 = 105 mm, L8 = 95 mm, l = 30 mm; Db = 10 mm;
– technological operations: milling the tube ends, drilling/reaming the pin holes;
– roughness of the machined surfaces: Ra1 = 12.5 µm, Ra2 = 6.3 µm;
– sharp edges are chamfered 1×45°;
– the position of the pin hole (and, if needed, of the adjustment pin hole) is set when drawing the assembly.
Adopted joint components
– spring-type (safety) split pin, d = 2.5 mm;
– washer for pins: d1 = 10 mm, D = 20 mm, h = 2.5 mm.