Design data
External forces: FX = 1500 N, FY = 300 N, FZ = 700 N act at distances Lc = 70 mm, X1 = 80 mm, X2 = 220 mm, X3 = 150 mm, Y1 = 550 mm, Z1 = 180 mm, Z2 = 150 mm; the forces and moments at the centre of joint 13-2 are:
FXs = FX/2 = 750 N,
FYs = FY/2 = 150 N,
FZs = FZ/2 = 350 N;
MX2s = FY (Lc + Z1)/2 + FZ Y1/2 = 230000 Nmm,
MY2s = FX (Lc + Z1)/2 + FZ (X1 + X2 + X3)/2 = 345000 Nmm,
MZ2s = FX Y1/2 + FY (X1 + X2 + X3)/2 = 480000 Nmm.
Dimensional constraints: dimensions of element 2: b2 = b13 = 120 mm, L = 90 mm, a = 15 mm.
Operating constraints: temperature T = (−30…40) °C; outdoor working environment with high humidity.
Design constraints: steel for mechanical construction.
Materials and heat treatments
For elements 2 (2′), the steel for mechanical construction E335 according to SR EN 10025-2 (STAS 500/2) is adopted.
Material properties
| Material | Heat treatment | Hardness [HB] | Yield strength | Ultimate tensile strength |
|---|---|---|---|---|
| E335 | – | – | σ02 = 335 MPa | σr = 480 MPa |
Sizing
Calculation data
– loading: FYs = 150 N, MX2s = 230000 Nmm;
– shape and dimensions: flat bar of width b2 = b13 = 120 mm; the thickness g2 is unknown;
– materials: σ02 = 335 MPa – the yield strength; σat = σ02/c = 335/(2…3) = (111.66…167.5) MPa – the allowable tensile stress (σat = 140 MPa is adopted); σaî = (1.05…1.1)σat = (147…154) MPa – the allowable bending stress (σaî = 150 MPa is adopted);
– bending moment in the critical section: Mîmax = MX2s + FYs Z2 = 230000 + 150·150 = 252500 Nmm.
Sizing
From the bending strength condition, with Mîmax = 252500 Nmm, b2 = 120 mm and σaî = 150 MPa,  = 9.2 mm; a flat-bar blank of standard thickness g2 = 10 mm and width b2 = 120 mm is adopted.
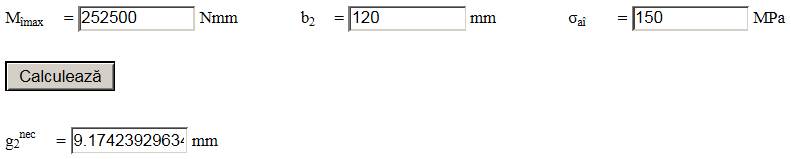
Constructive-technological shape
Constructive-technological drawing
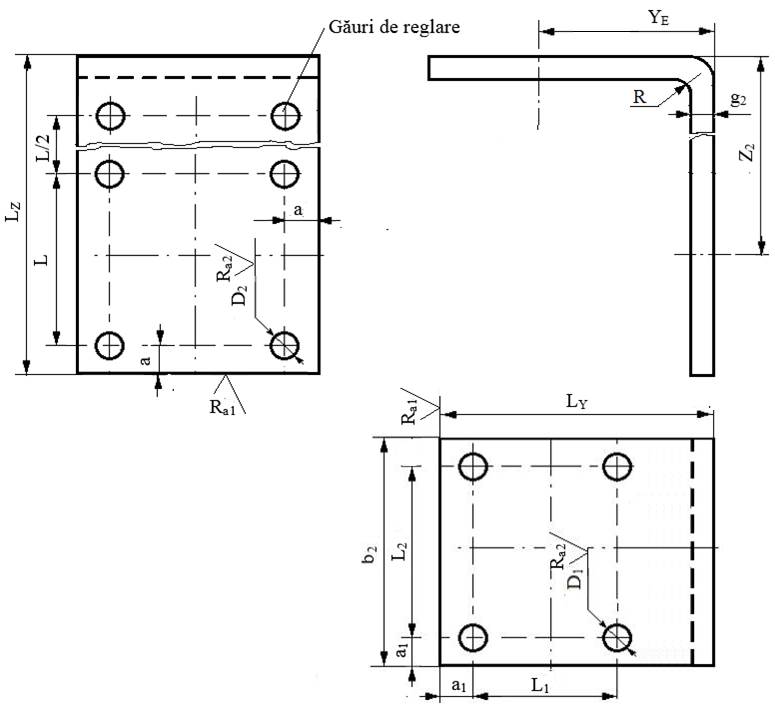
Adopted dimensions and constructive-technological parameters
– dimensions: Z2 = 150 mm, YE = 60 mm, b2 = 120 mm, g2 = 10 mm, a = 15 mm, L = 90 mm, R = 20 mm, LZ = 210 mm, LY = 120 mm, a1 = 15 mm, L1 = 70 mm, L2 = 90 mm; the other dimensions (D1, D2) result from the calculation of the bolt-nut joints (Bolt 1, Bolt 2);
– the number of sets of adjustment holes is set when drawing the assembly;
– technological operations: milling, bending, drilling; fillet radius in the bending zone R = 20 mm;
– sharp edges are chamfered 1×45°;
– roughness of the surfaces machined by milling or drilling: Ra1 = 12.5 µm, Ra2 = 6.3 µm.