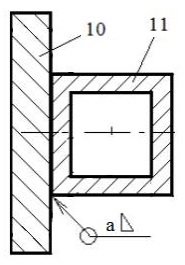
Design data
External forces: FX = 1500 N, FY = 300 N, FZ = 700 N act at distances Lc = 70 mm; X1 = 80 mm; Z1 = 180 mm and h6 = 60 mm, a = 140 mm, g = 10 mm; the bending moments at the centre of the flange (the welded joint) are:
MX10 = FY (Lc + Z1) = 75000 Nmm,
MY10 = FX (Lc + Z1) + FZ (X1 + h6/2 + a + 2g) = 564000 Nmm,
MZ10 = FY (X1 + h6/2 + a + 2g) = 81000 Nmm.
Dimensional constraints: flange 10 is welded to the central bar 11, with dimensions Lf = 120 mm, g = 10 mm, h11 = 60 mm, t11 = 5 mm.
Operating constraints: temperature T = (−30…40) °C; outdoor working environment with high humidity.
Design constraints: weldable materials for elements 10 and 11.
Materials and heat treatments
Elements 10 and 11 were designed in weldable S235 steel according to SR EN 10025-2 (STAS 500/2).
Material properties
| Material | Heat treatment | Hardness [HB] | Yield strength | Ultimate tensile strength |
|---|---|---|---|---|
| S235 | – | – | σ02 = 235 MPa | σr = 360 MPa |
Sizing
Calculation data
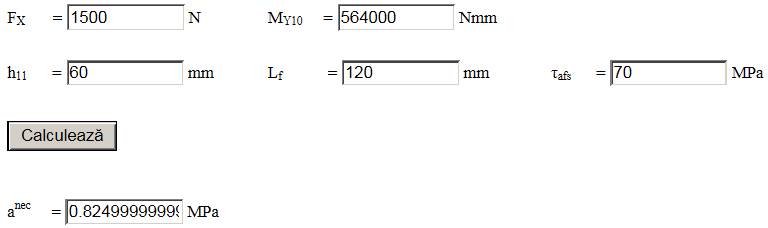
– loading: FX = 1500 N, MY10 = 564000 Nmm;
– shape and dimensions: the weld bead is rectangular, with dimensions Lf = 120 mm and h11 = 60 mm;
– materials: σ02 = 235 MPa – the yield strength; c = 2…3 – the safety factor; σat = σ02/c = (80…118) MPa – the allowable tensile stress; τafs = 0.65σat = 70 MPa – the allowable shear stress of the weld.
Sizing
From the sizing relation obtained from the shear strength condition of the weld, with FX = 1500 N, MY10 = 564000 Nmm, h11 = 60 mm and τafs = 70 MPa, the weld throat thickness is anec = 0.83 mm; a = 3 mm is adopted.
Constructive-technological shape
Constructive-technological drawing
|
Recommendations for choosing the dimensions and constructive-technological parameters: – weld throat thickness a = 3 mm; – the weld is made along the closed contour (as symbolised); – after welding, the subassembly undergoes stress-relief annealing. |